Top 10 Precision Steel Manufacturers Known for Consistent Quality and Dependable Supply
2026-11-16
Finding a precision steel supplier that consistently delivers both quality and dependable supply is harder than most buyers expect. In this ranking, we look beyond flashy claims to focus on manufacturers with proven production control and on-time performance. Among them, Shunchen steel stands out for its disciplined approach to tolerances and repeat orders. Here are the top 10 names worth shortlisting.
Why Consistent Quality Is Harder to Achieve Than It Looks
Most teams assume that once a process works, repeating it is just a matter of discipline. In practice, small shifts in raw materials, operator fatigue, ambient temperature, or even the way instructions are interpreted can push the same steps toward different outcomes. Consistency rarely fails because someone ignored a major rule; it erodes through dozens of tiny, almost invisible compromises that accumulate before anyone notices.
The harder part is that standards themselves decay. A checklist written six months ago may no longer match the tools, suppliers, or team members currently in place, but people keep following it because changing the document feels riskier than accepting the drift. Meanwhile, newer employees learn the exceptions along with the rules, so what gets passed down is a mix of the official process and informal workarounds. That blend becomes the real standard, and it is never exactly the same twice.
Inside the Mill Practices That Reduce Supply Chain Surprises
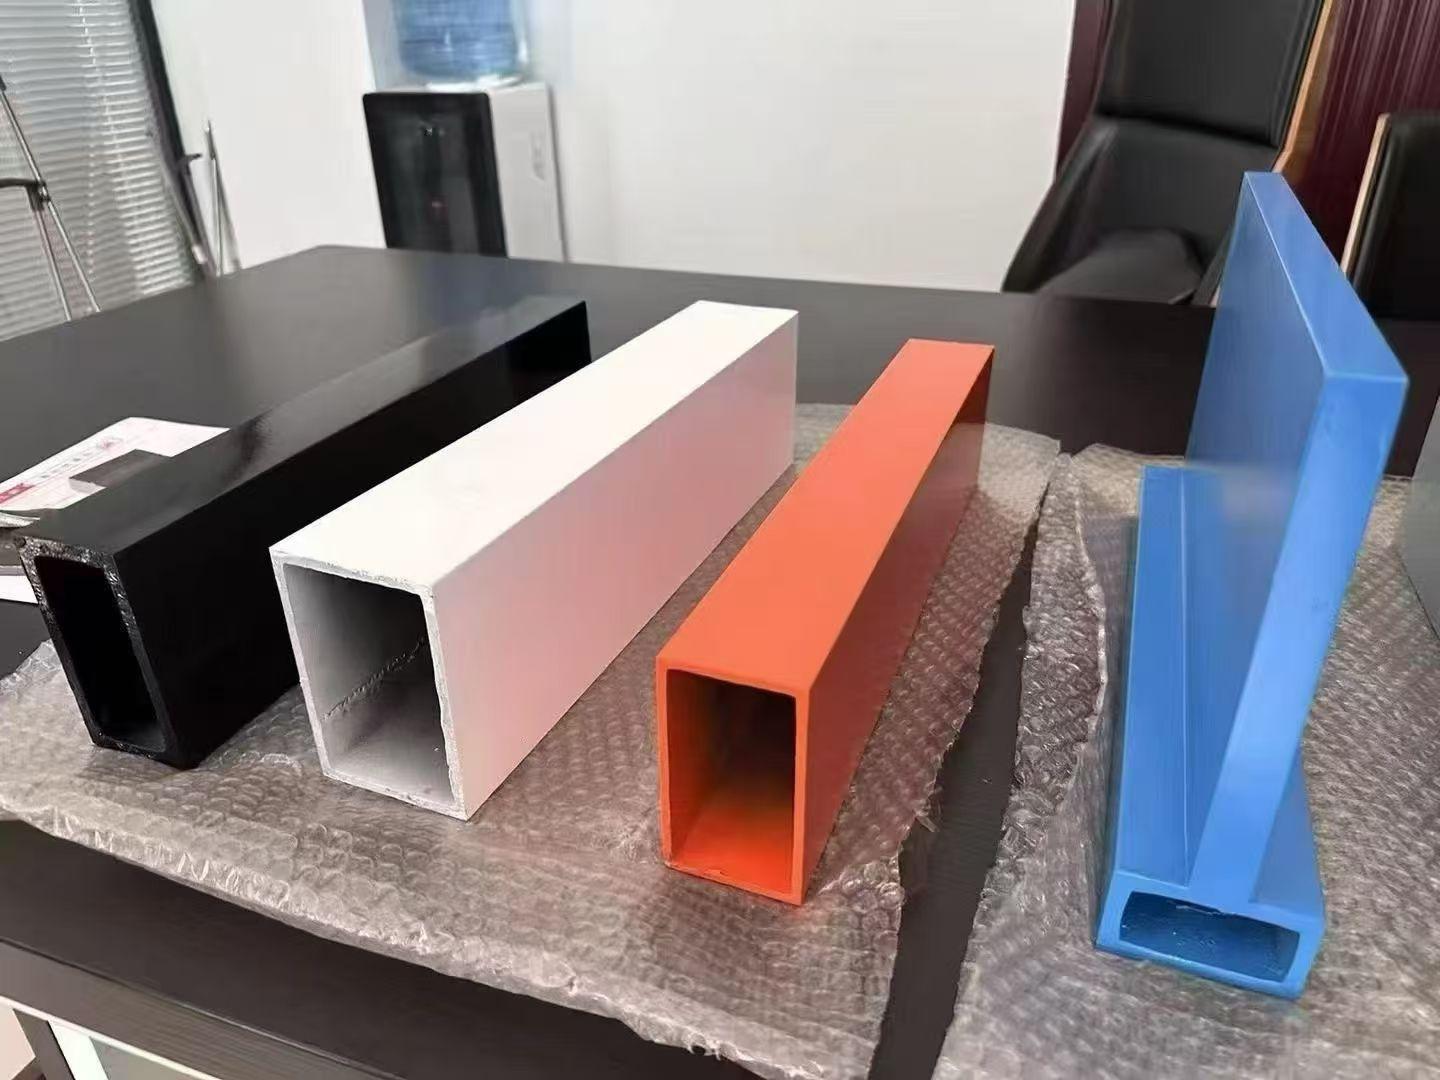
Most supply chain surprises don't start with a phone call from a freight forwarder. They start on the mill floor with a skipped calibration, a rushed batch change, or a moisture reading that gets written down but never acted on. The mills that stay boring—in the best way—treat those small signals as part of the production rhythm. Operators log each raw material lot against the purchase order and flag anything that drifts from the usual range before it becomes a downstream problem.
Blending and buffer capacity get most of the attention, but the quieter practices matter more. A few mills keep a small reserve of pre-screened fiber or feedstock near the line, not because they expect a shortage, but because it gives them time to react when a truck is late or a supplier sends an off-spec load. Maintenance schedules are tied to actual run hours instead of calendar dates, so equipment gets looked at when it needs it, not when the spreadsheet says so. That cuts the unplanned downtime that tends to wreck delivery promises.
The same thinking carries into finished goods. Instead of building to a forecast and hoping it matches orders, some production planners hold semi-finished inventory at the point where products still share common traits. Final customization happens only after a customer confirms the details. It sounds like a small shift, but it lets the mill absorb a last-minute order change without reworking everything or pushing other jobs out of sequence.
Tolerances, Certifications, and the Real Cost of Precision
A tolerance of ±0.0002 inches rarely shows up on a quote the way it shows up on the shop floor. Holding that band means temperature control, slower cuts, and a coordinate measuring machine waiting at the end of the run. It also means a batch can drift out of spec after lunch if the coolant warms up. So the price of a part isn’t just the metal and the machine time; it’s the inspection, the rejected pieces, and the habits a shop has built to keep thermal growth from eating half the tolerance.
Certifications add another layer that is easy to misunderstand. AS9100 or ISO 13485 might look like plaques on a wall, but they represent living paperwork: material certs, calibration logs, first-article reports, and audit trails that survive years after shipment. That overhead doesn’t cut metal, yet it changes how work moves through a shop. A certified process has to be repeatable and documented, which means fewer shortcuts and more people checking what others have already done.
The real cost of precision is often paid later, not up front. A slightly cheaper part that misses a hidden chamfer or shows micro-burrs can fail in a medical pump or a landing gear actuator. Rework, line stoppage, and field returns wipe out the savings quickly. Paying for the right tolerances and the right certifications is less about buying a tighter number and more about buying a lower chance of discovering problems after the part has left the building.
Where Dependable Supply Meets Fluctuating Raw Material Markets
Raw material costs rarely move in a straight line, and that unpredictability has a way of rippling through every downstream decision. When ore prices spike without warning or a key alloy becomes scarce, the usual response is to either absorb the shock or pass it on to customers. Neither feels good. A more practical stance starts with mapping exactly where your supply chain touches volatile inputs, then building small buffers where they matter most—not everywhere, just at the points where a delay would cascade the fastest.
Dependable supply doesn't mean pretending prices won't swing. It means having the visibility to see a swing coming a few weeks earlier than your competitors do, and the discipline to act on that signal without overcorrecting. Some teams lock in quarterly pricing for the materials they can predict and keep a flexible line for the rest. Others lean on long-standing relationships with mills and distributors who will hold inventory through a rough patch rather than renegotiate at the worst moment.
The real advantage comes from treating raw material volatility as a design constraint instead of an emergency that interrupts your schedule. When purchasing, production, and sales share the same outlook on price direction and lead time risk, decisions speed up. That shared view is what turns a fluctuating market from a source of friction into a place where a dependable partner quietly stands out.
Lesser-Known Metrics Buyers Use to Vet Steel Partners
Beyond tensile strength and price per ton, experienced buyers watch mill-specific data that rarely appears on a certificate. One is the spread between heat analysis and product analysis for residual elements like copper and nickel; a narrow, consistent spread often signals tighter scrap control and fewer downstream forming surprises. Another is the coil-to-coil gauge profile variance within the same order, because a small average tolerance can hide a bimodal pattern that jams roll formers.
Some purchasing teams track the time from a documented claim to a corrective action letter, not just the replacement credit. They also ask for monthly internal reject rates by product family, not overall plant averages, since broad numbers can bury trouble in a single gauge or width. A mill that shares this data without defensiveness tends to get longer contracts even when its base price is not the lowest.
Lead time consistency can matter more than the shortest quoted lead time. Buyers increasingly compare the promised date to the actual mill release date across six or twelve months, flagging suppliers whose average looks acceptable but whose tail risk causes unplanned line stoppages. The same applies to packaging integrity scores, where repeated edge damage on a small share of skids reveals handling problems before they become full rejection events.
How the Best Manufacturers Handle Custom Specifications
Top-tier manufacturers don't treat custom specs as deviations from a standard catalog—they build their entire quoting and production flow around the assumption that every order will shift in some way. When a revision comes in, the best shops route it through a single point of contact who can parse both the engineering intent and the shop floor reality. That person checks tolerances against existing tooling, flags any feature that would require a new fixture before the customer even asks, and sends back a marked-up drawing the same day. The goal isn't to say yes to everything; it's to close the gap between what's drawn and what can actually be machined, molded, or assembled without a hidden cost spike.
What separates these manufacturers is how early they pull custom requirements into the conversation. Instead of waiting for a formal RFQ, their engineers sit in on the customer's design reviews and ask the uncomfortable questions about wall thickness, surface finish callouts, and whether a tapped hole really needs to be blind. They maintain a living library of past deviations—oddball thread sizes, non-standard coatings, split-lot packaging—so a new request rarely starts from zero. More importantly, they document the rationale behind each custom choice. If a buyer leaves or a second shift takes over, the reasoning doesn't evaporate with them.
Finally, the best manufacturers treat every custom spec as a small contract with its own verification loop. They don't just inspect the final part against the print; they run a separate check against the original custom request to catch drift. If a tolerance was tightened to solve a fit issue, they confirm that the tightened tolerance actually resolved it. When a material was swapped for lead time, they track the field performance of that substitution for at least six months. This habit of closing the loop turns one-off custom work into a repeatable process—and it's why their customers stop asking for quotes and start asking for capacity.
FAQ
It usually comes down to process control. Top names rely on tightly managed melting, rolling, and finishing steps, along with in-line measurement systems that catch dimensional drift before it leaves the floor. They also tend to hold certifications such as ISO 9001 or IATF 16949 and back their product with clear mill test reports.
While rankings shift with market focus, a dependable shortlist often includes voestalpine, Nippon Steel, POSCO, Thyssenkrupp, ArcelorMittal, Sandvik, Tata Steel, Baosteel, JFE Steel, and SSAB. Each has built a reputation around tight tolerances and steady supply rather than one-off deliveries.
Buyers often request a history of first-pass yield, on-time delivery records, and sample batches from multiple production runs. Site audits help, but long-term data matters more because it reveals whether a mill can repeat its results when demand rises or raw material prices shift.
A large part of supply reliability is upstream. Manufacturers with long-term contracts for high-grade scrap, direct reduced iron, or alloying elements are less exposed to spot-market shocks. That stability allows them to keep output predictable even when global steel prices swing.
Tighter tolerances reduce machining time, material waste, and assembly failures. In automotive, medical, and aerospace work, even small deviations can force line stoppages or part rejection, so buyers pay attention to a mill's ability to hold specified thickness, width, flatness, and straightness from coil to coil.
The stronger ones treat supply as part of the product. They maintain safety stock for high-demand grades, offer flexible lot sizes, and use regional service centers to shorten lead times. Communication matters too: they flag potential delays early instead of leaving the customer to chase updates.
Often, yes. A slightly higher per-ton cost can be cheaper overall when it means fewer rejected parts, less rework, and uninterrupted production. Buyers in critical industries usually measure value by cost per usable part, not just the invoice price.
More mills are adding digital traceability, tighter carbon footprint reporting, and near-net-shape casting to improve consistency while lowering waste. Buyers increasingly expect that every coil carries full digital records from heat chemistry to final inspection.
Conclusion
Precision steel buyers quickly learn that repeatable chemistry and mechanical properties are not accidental, even at mills that advertise tight tolerances. The plants that earn a place among the top ten treat melting, roll pass design, and heat treatment as one connected process rather than separate departments. Their internal checks tend to be stricter than the minimums on a certificate, and lot-level records are detailed enough that a single coil can be traced back through every shift, heat, and finish pass. That is what keeps unexpected hardness drift or edge cracking from turning into a downstream line stoppage.
Raw material swings separate genuinely dependable suppliers from the rest. When scrap and alloy prices move sharply, stronger mills rely on pre-negotiated buffer stock and transparent pricing mechanisms instead of quietly widening tolerances or substituting grades. Buyers who vet these partners look past brochures at less glamorous data—on-time-in-full rates, dimensional capability indices, surface defect frequency per thousand feet, and how quickly a mill answers a custom tolerance request with real engineering input. A custom specification should feel like a routine conversation—hardness range, edge condition, flatness, and straightness clarified before quoting—so the steel that arrives matches the steel that was planned. In that context, the real cost of precision is not a higher unit price; it is the avoided rework, delayed shipments, and hidden sorting labor.
Contact Us
Contact Person: Max Zhou
Email: [email protected]
Tel/WhatsApp: +86 15712216177
Website: https://www.shunchensteelmaterial.com/