T-Shirt Bag Factory Innovations for Sustainable Custom Bags
2026-08-31
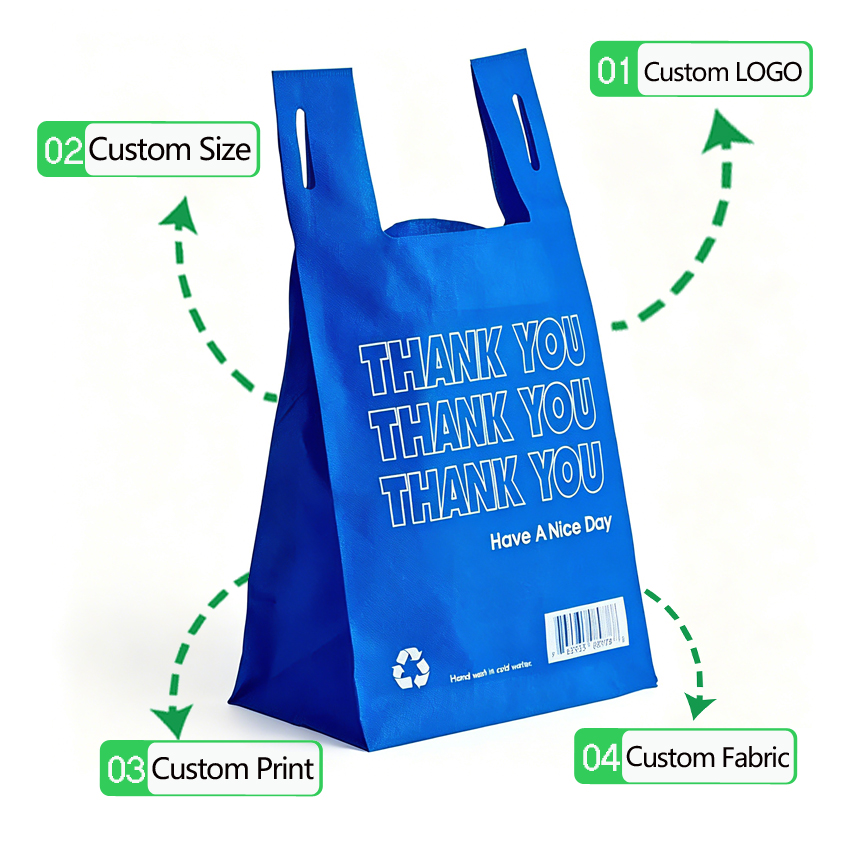
The humble T-shirt bag has come a long way from its basic plastic origins. Today, forward-thinking factories are reinventing this everyday item into a canvas for sustainable innovation—custom bags that blend practicality with environmental responsibility. As a leader in this shift, CHALLENGE WOLVES is rewriting the rules of what a simple bag can be, proving that eco-friendly production and bold customization can go hand in hand. In this post, we'll explore the latest breakthroughs from T-shirt bag factories and why they matter for your brand's next packaging move.
What Happens to Flawed Tees Before They Become Bag Panels
Flawed tees don't just get tossed into a pile and sliced up. First, they're spread out on long inspection tables under bright, unforgiving lights. Stains, small holes, uneven hems, misprinted graphics—each one gets marked with a wax pencil. Workers run their hands over the fabric to catch snags or weak spots that machines might miss. No two flawed shirts are alike, so every single piece is evaluated on its own, not by some rigid checklist.
Once the worst areas are circled, someone with a rotary cutter and a steady hand cuts away the damaged sections. It's not a perfect science—often the usable fabric is an odd shape, like a lopsided rectangle or a triangle with a curved edge. These leftover chunks are stacked according to rough size and thickness. Then they get pressed flat under heavy weights for a day or two. That step matters more than you'd think; a wrinkled tee won't feed through the panel-cutting die cleanly, and you end up with jagged edges that won't sew into a decent bag.
After pressing, the fabric pieces are grouped into small bundles, usually six to ten layers thick. The cutter uses a chalk outline or a metal template to trace the final bag panel shape—often a simple rectangle or a slightly tapered trapezoid. What's left after the cut is brushed off and collected for smaller projects like patch pockets or key fobs. So by the time a flawed tee becomes a bag panel, it has already passed through human hands at least three times, each step discarding a little more of what made it unsellable in the first place.
Cutting Patterns That Leave Almost No Offcut Behind
Efficient cutting starts long before the saw touches the material. Instead of treating each piece as a separate rectangle on a standard sheet, the most productive workshops use nested layouts that interlock curved and straight parts like a jigsaw. By clustering smaller components inside the negative spaces left by larger ones, the amount of leftover scrap drops dramatically, sometimes to less than three percent of the original board.
A different approach relies on shared cut lines. When two parts share an edge, a single pass separates them without creating a strip of waste between. This works especially well for rectangular or polygonal shapes that can be aligned edge-to-edge. With the right arrangement, the final cut frees both pieces at once, and the only remaining offcuts are thin slivers from the outer boundary.
Some fabricators go further by designing the product around the material dimensions. If a standard sheet is 2440 by 1220 millimetres, panel sizes are chosen so that the sheet divides into whole numbers with minimal kerf loss. That small shift in design thinking often removes the need for secondary trimming and turns what would have been waste into usable parts.
Why Low-Temperature Dyeing Keeps Cotton Fibers Stronger
Heat is one of the quietest enemies of cotton. When dyeing temperatures climb too high, the cellulose chains that give cotton its natural resilience begin to weaken. Prolonged exposure to near-boiling water can cause the fiber walls to swell unevenly, leading to micro-tears that later show up as pilling or premature wear. Low-temperature dyeing, by contrast, works below the point where cotton starts to lose its structural integrity. The dye molecules are still able to bond with the fiber, but the gentler thermal environment means the cotton retains more of its original tensile strength and elasticity.
Another advantage shows up in the hand feel. Cotton dyed at lower temperatures tends to emerge from the dye bath with a smoother, less rigid surface. High heat can strip away some of the natural waxes and pectins that sit on the outer layer of the fiber, leaving it brittle and rough. A low-temperature process preserves more of that protective coating, so the fabric keeps a softer, more supple drape right off the production line. This also reduces the need for aggressive finishing chemicals that are often used to compensate for heat damage.
From a production standpoint, the relationship between temperature and fiber strength is a simple equation: less thermal shock means fewer weak points. Dyers who shift to lower-temperature reactive dyes often report fewer breakages during subsequent wet processing and sewing. The cotton doesn't just feel stronger in the lab; it behaves stronger on the factory floor. That translates into better fabric yield, fewer rejections, and a final garment that holds its shape and surface longer for the end user.
Reinvented Handles That Skip the Plastic Core
Instead of wrapping a molded plastic skeleton in a thin veneer, these redesigned grips use a solid billet of bamboo, recycled aluminum, or dense cork as the load-bearing spine. The result is a handle that feels warmer in the hand and doesn't flex under heavy use.
The switch eliminates a common failure point. Traditional cores crack at the screw bosses after repeated impact, but a single-piece wooden or metal core spreads stress evenly. Makers can also shape the grip more organically, adding subtle palm swell and finger grooves that would be impossible over a bulky plastic insert.
You notice the difference the moment you lift the tool or pan. There's no hollow rattle, no seam where the outer shell meets a cheap core. The handle ages gracefully, picking up a patina instead of peeling, and when it finally wears out, it can be sanded down or recycled rather than sent to a landfill.
Small-Batch Printing That Keeps Deadstock Out of Landfills
Most print runs start with a guess: how many units will sell? Order too many, and the extras become deadstock—bolts of fabric, stacks of tees, or rolls of paper that nobody asked for. Small-batch printing flips that logic. Instead of producing thousands of items up front, you print closer to actual demand, often after an order is placed. That means fewer boxes sitting in a warehouse, fewer markdowns to clear inventory, and less material headed to a landfill simply because a forecast was off.
There's a second benefit that rarely gets mentioned. Deadstock isn't just unsold finished goods; it's also the leftover yardage from mills and garment factories. Small-batch printing works well with these remnants because you don't need huge quantities of any single fabric. A printer can take 50 yards of a discontinued weave, pair it with a limited-edition design, and turn what would have been waste into something people actually want. The constraint of small runs forces more thoughtful design, and the result often feels more special than another mass-produced drop.
This approach also changes the math for new designers and small studios. They can test a pattern with 30 units instead of 300, learn what resonates, and then decide whether to reprint. If a design flops, the loss is a few dozen pieces, not pallets of unsold product. Over time, that adds up to a meaningful reduction in textile waste—and a business model that doesn't depend on guessing games.
The Quiet Return Loop From Print Shop Scraps to Tote Lining
Most print shops sweep their offcuts into the recycling bin and call it a day. But a small group of binderies and studio printers started keeping the long, narrow strips left over from trimming posters and art prints. Those scraps, often too thin for most reuse projects, turn out to be perfect for something else: the hidden inner layer of everyday tote bags.
The process is slower than tossing waste into a single-stream bin. Scraps are sorted by fiber length, lightly heat-pressed to remove curl, and then layered between the outer canvas and a thin cotton liner. The result is a tote that carries a quiet history — a misprinted gig poster, the edge of a wedding invitation run, leftover color tests from an artist's edition.
Because the lining stays out of sight, there is no need for bleaching or heavy dyeing. That keeps water and chemical use low, while giving the scraps a second life that never has to be announced. The return loop is small, local, and rarely mentioned — but every completed tote keeps a few more pounds of coated paper from ending up in a landfill.
FAQ
We start by sorting cotton-rich tees, removing buttons and seams, then shredding and re-spinning the fibers. The resulting fabric is cut and sewn into bag panels that hold up to daily use without feeling flimsy.
Instead of shipping in new cotton or polyester, the factory runs a closed-loop system. Scraps from cutting are collected, blended with recycled plastic bottles, and turned into durable handles or bottom gussets, so almost nothing leaves as waste.
Yes, the factory keeps a stock of pre-dyed, low-impact base fabrics. You can order as few as 50 bags and still choose from water-based inks or natural dyes, which don't require large chemical baths to set the colors.
Water-based screen printing and digital textile printing are the go-to options. Both skip heavy solvent use, and the factory's heat-curing step runs on solar power during daylight hours, cutting energy draw significantly.
Each batch of reclaimed cotton goes through a color-sorting stage before spinning. The factory keeps control swatches from previous runs and blends fibers proportionally, so the final bag color stays within a tight tolerance without adding synthetic dyes.
Reinforced stitching, interior slip pockets, and cotton webbing handles are all safe choices. The factory avoids plastic zippers and vinyl labels, instead offering embroidered patches or stamped cork tags that can be removed before composting.
The cotton-only versions, with cotton thread and untreated cork tags, break down in home compost within six to nine months. Blended bags with recycled polyester handles take longer and are better suited for textile recycling drop-offs.
Low-liquor dyeing machines cut water use by about 40 percent compared to traditional vats. Rainwater collected from the factory roof is filtered and reused for the first rinse cycle, and leftover dye water is treated on-site for reuse in non-critical cleaning.
Conclusion
At the heart of these bag factories is a simple shift in mindset: nothing gets wasted unless you stop paying attention. Flawed tees that would normally sit in a reject pile are sorted by fabric weight and color, then cut into panels that become the body of a custom tote. The cutting tables are designed around modular patterns—some pieces interlock like puzzle fragments so that leftover scraps from one bag turn into gussets, pocket linings, or even narrow binding strips. That level of precision means offcuts are often measured in centimeters, not meters, and the few scraps that remain are baled for the next round of recycling.
Low-temperature dyeing plays a quieter but equally important role. Because the cotton isn’t shocked by boiling water, the fibers keep more of their natural twist and tensile strength, so the finished bags hold up longer and need replacing less often. Handles have been reimagined too—instead of wrapping foam or plastic inserts inside fabric tubes, many shops now use layered cotton selvage or tightly rolled scrap yarn to give the strap enough body without hidden synthetics. When a print shop overruns a design or produces a misregistered sample, those printed panels don’t get tossed. They come back through a return loop, get trimmed and sorted, and end up as linings inside tote bags. Small-batch printing then keeps the whole system honest: only what’s ordered gets made, which means deadstock never piles up in the first place.
Contact Us
Contact Person: Tony
Email: [email protected]
Tel/WhatsApp: +8615859766913
Website: https://www.cw-pak.com