China Video Measuring Machine: Precision Inspection for Modern Manufacturing
2026-10-01
Precision inspection has never been more critical—or more demanding. Video measuring machines from China are rewriting the rules of quality control, combining speed, accuracy, and ease of use in ways traditional methods simply can't match. For any manufacturer serious about zero-defect production, the question isn't whether to adopt this technology, but which system to trust. That's where JATEN comes in. Built for the realities of modern shop floors, JATEN's solutions make high-precision measurement accessible without the usual complexity. Read on to see how the right machine can transform your inspection process from a bottleneck into a competitive edge.
Where Microns Matter Most
In precision manufacturing, the difference between flawless performance and catastrophic failure often hides in measurements smaller than a human hair. A few microns can decide whether a fuel injector atomizes perfectly or dribbles wastefully, whether a bearing spins silently for decades or grinds itself to dust in weeks. It's at this scale that material choices, thermal expansion, and surface finishes stop being abstract specs and start dictating real-world reliability.
Consider the humble hydraulic valve. Shift its spool clearance by three microns and you've traded a tight seal for internal leakage that quietly bleeds efficiency. Do the same inside an optical lens mount and thermal drift becomes your permanent enemy, throwing focus off by millimeters at the sensor. These are not defects you catch with a caliper or a quick visual check—they demand interferometers, air gauges, and patience.
What separates top-tier workshops isn't just better machines, but a stubborn refusal to shrug off deviations that most would call negligible. They know that when you're chasing microns, every fixture, every temperature fluctuation, and every tool wear pattern matters. The reward isn't a prettier part; it's a component that quietly outperforms every expectation once it's buried inside a larger system.
The Camera That Never Blinks
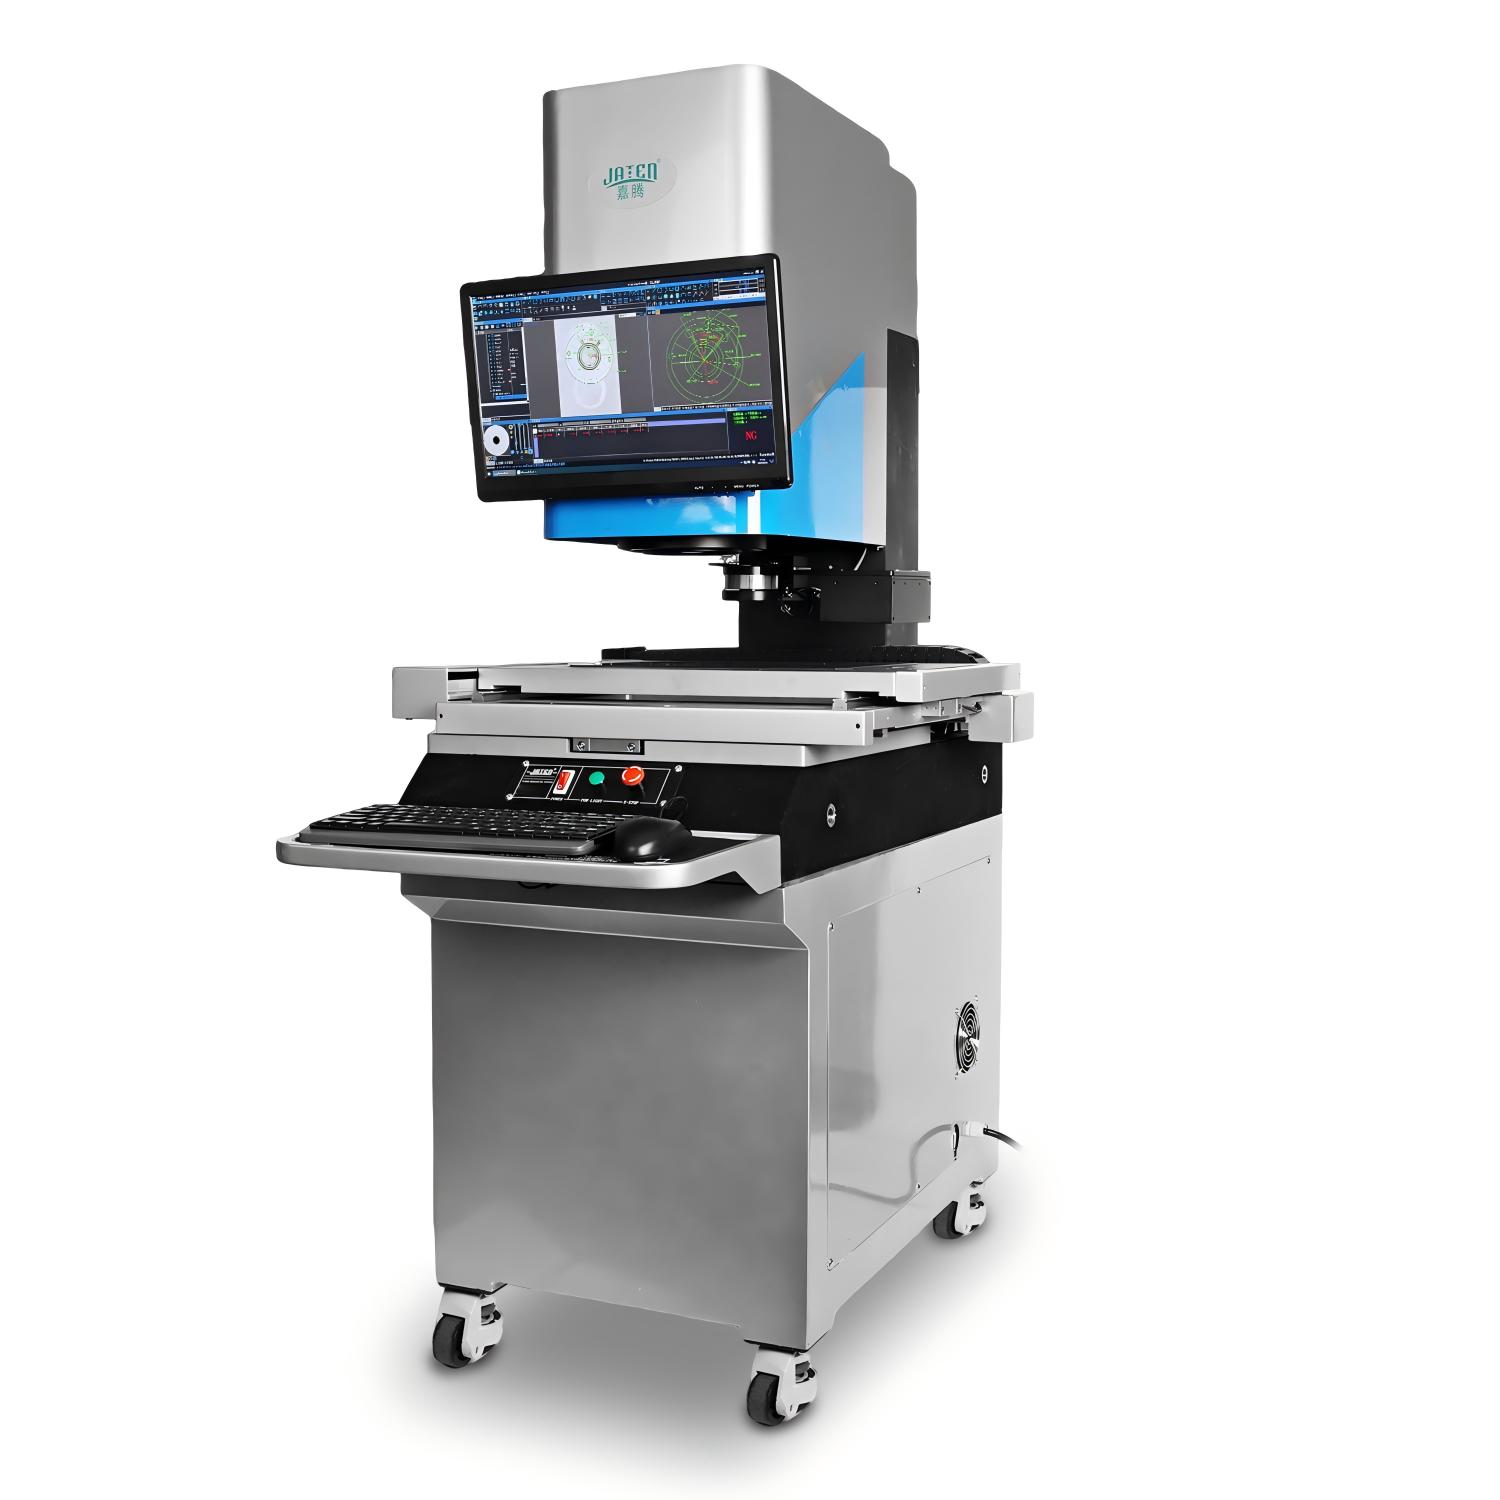
A lens fixed on a street corner, a hallway, a train platform. It doesn't sleep, doesn't glance away, doesn't pause for breath. The camera that never blinks has settled into the background of daily life, quietly logging the ordinary and the unexpected. Its patience is not human. It doesn't grow bored or distracted. It waits through empty hours, through rain and glare, through the slow drift of shadows, until something moves that shouldn't—or until a rare moment finally appears.
Removing the blink changes what gets remembered. A blink is a tiny reset, a fraction of a second when the world disappears. Without it, every frame runs into the next, leaving no seam for a missed detail. That matters in a security room where a split-second handoff can be the whole story. It matters on a mountain pass where an avalanche starts with a whisper of snow. And it matters in a wildlife reserve where a species thought gone steps into the open only once in a decade. The unblinking eye doesn't guarantee understanding, but it refuses to look away.
The machinery behind this constant gaze is often less dramatic than the idea. A sensor tuned to low light, a shutter that never closes, a feed that pours into storage. But the deeper shift is in how people move and speak when they know the pause between frames has been eliminated. A camera that never blinks is not just a recorder. It is a quiet assertion that every second might be the one worth keeping.
Mapping Surfaces in Seconds
The moment you press the scan button, the device starts throwing invisible patterns across the object in front of you. Within two or three heartbeats, those distorted lines are translated into a dense point cloud that reconstructs every groove, bevel, and curve. There is no waiting for a desktop workstation to crunch the data; the mapping happens right on the handheld unit, letting you walk around a part and see the surface build itself in real time.
What makes this speed possible is a shift away from stitching dozens of static photographs. Instead, the system tracks its own position relative to the surface, fusing depth frames on the fly. That means you can sweep across a car door, a sculpture, or a worn machine housing without pausing to reset the scanner or place markers. The software quietly resolves overlaps and fills small occlusions, so the final mesh feels continuous rather than assembled from separate patches.
For anyone who has spent hours with older tools—moving a probe point by point, or waiting for a turntable to inch through its rotation—the difference is immediate. You stop thinking about the scanning process and simply move your hand the way you would with a spray can. The surface appears as a live preview, and when you lower the device, the mapped geometry is already sitting there, ready to be exported or refined.
From Castings to Circuit Boards
The jump from pouring iron into sand molds to laminating copper onto epoxy sheets feels almost like switching trades entirely, yet plenty of shops have made exactly that move. Old foundry floors once measured success by the weight of a pour and the patience of a cooling casting; now the same square footage might hold a pick-and-place machine placing resistors the size of pepper flakes.
Casting tolerances came from draft angles, shrinkage rates, and the steady hand of a grinder. Board work, in contrast, leans on photoresist chemistry, etchant baths, and solder paste that barely holds its shape before reflow. The materials barely share a vocabulary: cast iron and aluminum gave way to FR-4, polyimide, and traces thin enough to hide under a fingerprint. Even the rejects look different—porosity and cold shuts versus solder bridges and tombstoned parts.
That doesn't mean the old skills vanish. A good process engineer still reads thermal behavior, just in a reflow oven instead of a cooling flask. The real throughline is controlling how materials behave when heat, pressure, and timing collide, whether the result is a pump housing or a motor controller tucked inside it.
China's Answer to Precision Demands
Precision manufacturing has long favored established players, yet China's approach flips the script by blending state-backed infrastructure with agile, application-driven engineering. Instead of merely chasing tolerances for their own sake, domestic firms target specific pain points in sectors like EV batteries, surgical tools, and aerospace fasteners—where micron-level consistency directly translates to safety and performance. This focus has spawned hybrid production models that pair imported metrology with locally developed adaptive control software, yielding setups that learn from each batch rather than relying on static specs.
A case in point is the rise of modular precision cells in the Yangtze Delta, where small-batch makers share calibration data through regional industrial networks. Rather than each factory investing in expensive climate-controlled labs, they lease time on community-grade coordinate measuring machines and collectively refine process windows. The result is a precision ecosystem that behaves more like an open-source project than a collection of trade secrets—mistakes are cataloged, fixes are versioned, and best practices spread quickly across supply chains.
What distinguishes this from older catch-up strategies is an emphasis on repeatability under real-world conditions. Chinese engineers increasingly test for thermal drift, vibration, and material variability in the same environments where components will actually run, not in idealized labs. That shift—from theoretical accuracy to dependable accuracy—addresses the frustration many global buyers have with precision parts that pass inspection but fail in the field. By treating precision as a systemic challenge rather than a machine specification, China's manufacturing sector is redefining what 'good enough' means for high-stakes applications.
Quality Gates That Run Themselves
Traditional quality gates tend to rely on a human approving at each stage, which creates bottlenecks and inconsistent decisions. A gate that runs itself replaces that manual checkpoint with automated policies and real-time telemetry. The pipeline checks test coverage, vulnerability scans, performance budgets, and configuration drift before promoting a build. If a metric falls outside the allowed range, the release pauses and the responsible team gets a concise alert with the exact failing condition—no meeting, no ticket shuffle.
The trick is making the thresholds meaningful rather than ceremonial. Start with two or three signals that have caused production incidents in the past, such as p95 latency or error rate on canary deployments. Then encode those as numeric guardrails that can be evaluated automatically. Let the gate observe a canary for a set window and compare it to the previous release, rather than asking someone to eyeball a dashboard.
Once these gates earn trust, teams stop treating deployment as a high-stakes event. The system can even auto-rollback when a canary metric degrades, which closes the loop without waking anyone up. Over time, the gates become quieter because failures are caught earlier and fewer bad builds reach the later stages.
FAQ
A video measuring machine uses high-resolution cameras and precision optics to capture dimensions of components without physical contact. It's essential because it ensures parts meet tight tolerances quickly, reducing errors in high-volume production.
They typically integrate linear scales, granite bases for thermal stability, and advanced image processing algorithms. Many factories also conduct rigorous calibration against certified standards before shipping.
Electronics, automotive, aerospace, and medical device sectors rely heavily on them. Any industry producing small, intricate parts with strict quality requirements finds them indispensable.
Not entirely. While video systems excel at fast, non-contact inspection of delicate or tiny features, contact probes remain useful for deep holes or very specific surface roughness checks. Many systems now combine both methods.
A video measuring machine relies on optical imaging and is generally faster for 2D measurements, while a CMM uses a physical probe and handles complex 3D geometries better. Video machines are often more affordable and simpler to operate.
Consider the size of parts, required magnification, measurement accuracy, and whether automation features like programmable stages are needed. Also evaluate the software's ability to handle edge detection and reporting formats.
Yes, they offer a strong balance of performance and cost. Many Chinese manufacturers have adopted advanced components like imported lenses and controllers, while providing local service and customization that appeals to global buyers.
Regular cleaning of lenses and stages, keeping the environment dust-free and temperature-stable, and conducting periodic recalibration with gauge blocks are key. Software updates also help maintain measurement consistency.
Conclusion
China's video measuring machines have become indispensable where tolerances shrink to a handful of microns—think turbine blade profiles, connector pins, or injection-molded gears. Instead of a conventional touch probe, these systems pair a high-resolution camera with sub-pixel edge detection, so the camera that never blinks catches burrs, dust, or tool wear that a coordinate measuring machine might miss or take minutes to reach. The stage movement and lighting are synchronized to map entire surfaces in seconds: a 200 mm × 200 mm part can yield thousands of measurement points before an operator finishes loading the next fixture. That speed changes how factories handle everything from rough castings to densely populated circuit boards, where via positions and pad geometries demand both speed and consistency.
This shift is China's direct answer to precision demands coming from EV powertrains, consumer electronics, and medical devices. Rather than exporting measurement work to separate labs, manufacturers install these machines right at the line, turning inspection into quality gates that run themselves. Automated programs recall part-specific scripts, adjust lighting per feature, and flag trends like drift in a molding tool before defects escape. The result is a tighter loop between machining and correction—less scrap, fewer rework batches, and a production record that auditors can trace. In many plants, the video measuring machine no longer sits in a metrology room; it stands beside the CNC, quietly deciding what ships and what gets sent back.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/