Best DIP Switch Manufacturer: Key Factors to Evaluate Quality and Reliability
2026-09-09
Sourcing DIP switches might seem like a minor decision, but the wrong choice can quietly undermine an entire product. Quality and reliability hinge on details most buyers never think to check—contact plating, housing material, even the consistency of the actuator feel. This article walks through the key factors that separate dependable manufacturers from the rest, using real-world failure modes to show why shortcuts backfire. Among the names worth a closer look, KEJIAN ELECTRONICS has built a reputation for addressing these pitfalls head-on, without the usual marketing gloss.
Material Selection Tells You More Than a Spec Sheet
A spec sheet gives you tensile strength, density, and thermal conductivity, but it won't tell you how a material behaves when a corner gets nicked during assembly or when the ambient temperature swings from freezing to blistering over a single afternoon. Real selection means digging into fatigue life under cyclic loading, creep resistance at elevated temperatures, and the way a polymer's impact toughness drops after a few hundred hours of UV exposure. Engineers who rely solely on published numbers often find their prototypes failing in ways the datasheet never predicted, because the lab conditions behind those figures rarely match the messy reality of a product's life.
The hidden half of material choice involves the supply chain and the shop floor. A corrosion-resistant alloy might look perfect on paper until you discover it requires a specialist welder, a three-month lead time, or a minimum order quantity that blows your budget. Machinability, formability, and even the consistency of heat treatment from batch to batch can make or break a project faster than any spec sheet metric. Many teams learn this the hard way when a beautiful design stalls because the chosen material can't be anodized uniformly or tends to warp during cooling.
Then there's the growing list of non-engineering factors that never show up in a standard datasheet: recycled content, end-of-life recyclability, conflict-mineral reporting, and whether the supplier will survive your product's warranty period. Choosing a material today also means choosing a story about where it came from and where it will go. The spec sheet stays silent on all of that, which is why experienced teams treat it as a starting point for conversation, not a decision document.
How Consistent Are the Detents Across a Single Tube?
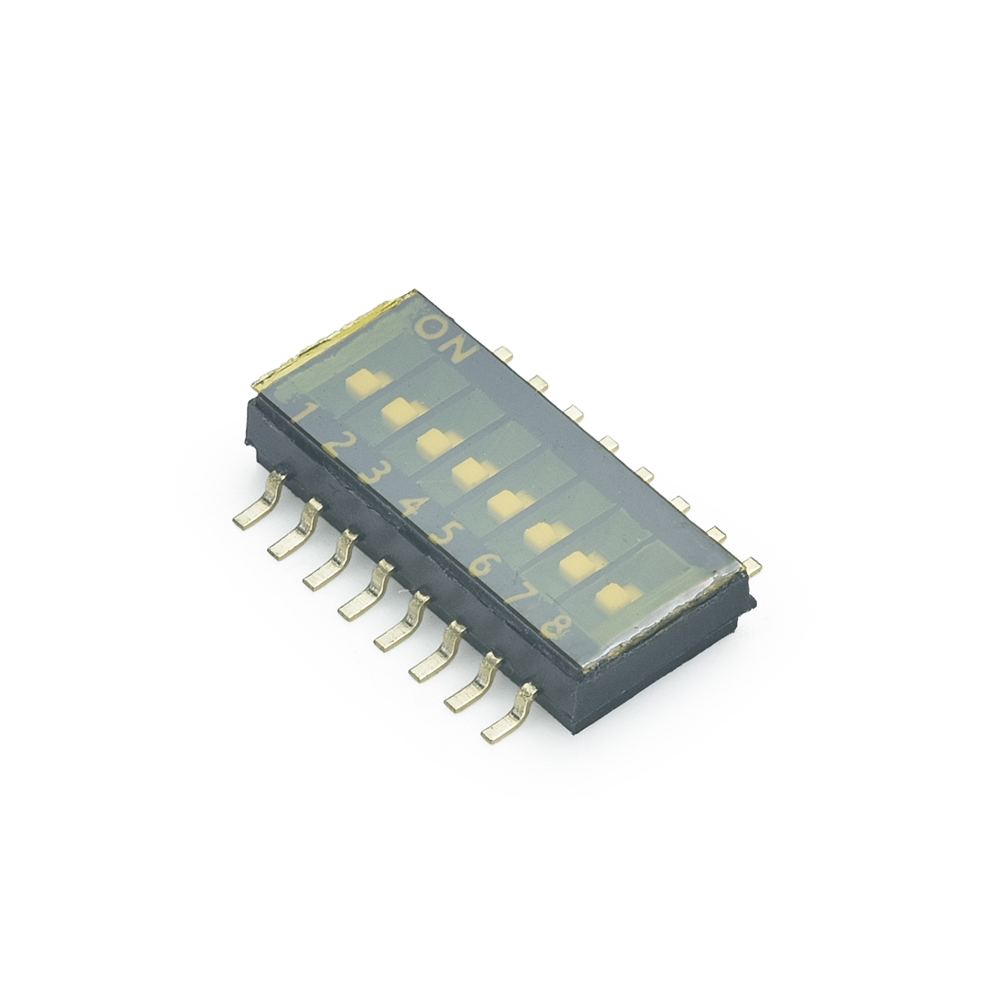
When you look closely at detents within a single tube, the consistency often comes down to how the tube was formed. Processes like rotary swaging or internal broaching can leave subtle variations—sometimes a few thousandths of an inch—between detents that are supposed to be identical. These differences aren't always visible to the naked eye, but they show up when you test engagement force or run a mating pin through each position.
A practical way to check consistency is to use a spring-loaded plunger and measure the pull-out force at each detent. In a well-made tube, you might see force readings within a 10% band across all detents; in a poorly controlled batch, that band can easily double. The location along the tube's length also matters—detents near welded or heat-affected zones often behave differently due to localized hardening or distortion.
For most applications, what you really need is not perfect uniformity but predictable performance. If the detents are consistent enough to avoid accidental release under normal vibration and still allow intentional adjustment without excessive force, the tube is doing its job. Engineers often specify a tolerance window for depth and spacing rather than expecting micrometer-level repeatability, because real-world manufacturing always involves a trade-off between cost and precision.
Plating Thickness and the Hidden Cost of Corrosion
When engineers specify plating thickness, they often focus on immediate performance metrics like wear resistance or electrical conductivity. Yet the real financial burden rarely shows up on the initial invoice. Thinner coatings may pass a salt spray test for a few hundred hours, but once the underlying substrate begins to corrode, the repair costs escalate far beyond the savings from using less material. A seized fastener on an offshore platform or a pitted contact in an automotive harness can trigger weeks of downtime and secondary damage that no plating quote ever accounted for.
The hidden cost doesn't stop at replacement parts. Corrosion byproducts can migrate into adjacent assemblies, causing galvanic incompatibilities that were never present in the original design. Rework in the field often requires disassembling components that were never meant to be serviced, and each labor hour spent chasing a rust trail is an hour not spent on productive output. Plating thickness acts as a time buffer: every additional micron delays the inevitable, and that delay translates directly into fewer unscheduled outages.
Smart buyers now look beyond the per-unit plating price and ask a different question: what does a premature failure actually cost in my specific application? The answer usually dwarfs the material difference between a 5-micron and an 8-micron coating. By treating corrosion as a lifecycle expense rather than a cosmetic nuisance, design teams can justify the upfront investment in a more robust plating specification and avoid funding the far more expensive failures later.
Beyond Rated Cycles: What Happens at Year Three?
The sticker on the pack says 1,000 cycles, maybe 80% capacity remaining. But nobody runs a controlled lab discharge at year three. Real use piles up partial cycles, high temperatures, fast charging, and the occasional deep discharge. By month 36, the cell's internal resistance has climbed enough that the voltage sags under load, even when the state-of-charge looks fine. That sag triggers early low-battery warnings and forces the battery management system to throttle power, not because capacity is gone, but because the chemistry can't push current the way it did when new.
Calendar aging quietly stacks on top of cycle aging. The electrolyte keeps reacting at the anode, thickening the solid-electrolyte interphase. You can't see it in a cycle counter, yet it steals usable lithium and raises impedance. At year three, cells that were never pushed hard still lose capacity just from sitting at high state-of-charge in warm weather. Two identical packs can drift apart: one cycled gently in a cool garage, another fast-charged daily in Phoenix. Their rated life looks similar on paper, but the real-world gap at year three is often larger than the datasheet suggests.
Then comes the failure curve's shallow climb. Not catastrophic, just annoying: one cell in a series string drifts low first, the balancer works harder, heat builds up in corners, and range or runtime slips another percent every few weeks. Replacement decisions get harder because the pack still works, but it no longer fits the daily routine. Year three is where rated cycles stop being a promise and start being a memory.
Traceability That Actually Reaches the Raw Plastic
Most recycling claims stop at the baler or the pellet silo, but that leaves a huge blind spot: the exact origin and composition of the raw plastic feedstock. Tracing a finished product back to a batch of mixed flakes tells you little about which suppliers, which production runs, or which resin lots actually entered the stream. Real traceability means linking every granule to a specific input—whether it's post-consumer bottle scrap from a single collection route or industrial scrap from a known injection molding line—without relying on averages or assumptions.
The practical way to achieve this is by embedding unique identifiers at the earliest possible stage. Instead of tagging bales or gaylords, some processors now add microscopic tracer particles directly into the shredder feed or use spectroscopic fingerprints captured before extrusion. Each batch of raw plastic carries a digital signature that follows it through washing, sorting, and pelletizing. When a downstream molder scans a finished part, the system retrieves the exact lot numbers, source locations, and even the original collection dates—down to the truck that delivered the scrap.
This level of granularity changes how brands and converters handle audits. Rather than presenting a generic certificate stating "contains 30% recycled content," they can pull up a live map of every raw plastic input, with timestamps and mass balances that match the physical inventory. If a contaminant shows up in a final product, the traceback doesn't stop at "post-industrial polypropylene"; it pinpoints the specific regrind batch from a supplier in Ohio that failed a melt-flow test three weeks earlier. That kind of accountability is what finally makes recycled plastic a trustworthy engineering material, not just a marketing checkbox.
What Their Rejection Rate Says About Final Inspection
A supplier’s rejection rate is often read as a simple performance score, but in final inspection it works more like a pressure gauge. A low figure may suggest mature processes yet can also hide loose in-house checks that push problems downstream. A high figure, while unwelcome, at least means the inspection step is not being bypassed.
The real value shows up when rejection data is matched against defect categories and timing. If the same nonconformities keep appearing at final inspection, the rejection rate is not just measuring product failure; it is exposing a broken corrective action loop. In that light, the number ceases to be a scorecard and becomes a diagnostic tool.
Teams that only chase a lower rejection rate often end up weakening the final inspection itself. Pressure to pass borderline units can quietly erode acceptance standards. What matters is not the rate in isolation, but whether each rejected batch triggers a specific change upstream. That is what turns a rejection statistic into evidence of a functioning quality system.
FAQ
Ask for a tear-down of a switch that has survived at least 50,000 cycles under load. The internal contact shape tells you more than the datasheet. Look for sharp, consistent wiping action and no signs of pitting on the copper alloy. Also check whether the actuator molding has flash or uneven parting lines; that often predicts how the switch will feel after two years in the field.
Thin gold flash over nickel is a common weak point. If the gold layer is under 0.4 microns, repeated switching quickly wears through to the nickel, raising contact resistance. Avoid switches with a single point of contact; a bifurcated or cross-bar contact spreads wear and keeps resistance stable far longer. Cheap thermoplastic actuators also deform under heat, causing intermittent contact.
Run ten samples through a standard reflow profile twice, then measure each pole's contact resistance at both end positions. A spread greater than 20 milliohms across samples usually means the internal spring lost temper or the housing warped. Another quick test: press the actuator down at a 15-degree angle. If the switch clicks unevenly or sticks, the internal rocker is not seating properly.
The gap between the actuator and housing is critical. Too tight and solder flux gets trapped; too loose and vibration causes the actuator to bounce off the contact. Look for manufacturers that specify a clearance of 0.05 to 0.15 mm and use ultrasonic welding rather than snap-fit covers. Welded housings keep the internal spring preload consistent, which prevents chatter.
Not for switches that are set once and sealed inside an enclosure. For those, a 0.8 micron tin-lead or bright tin finish over a nickel barrier is usually enough. Gold pays off when the switch is re-adjusted often, operates in a corrosive atmosphere, or carries low-level signals below 100 mA. In those cases, insist on at least 0.8 microns of hard gold over 2 microns of nickel.
Missing actuation force graphs, vague temperature ratings like standard industrial range, or no mention of the base material. Also be wary if the datasheet lists only initial contact resistance with no end-of-life value. A reputable factory will specify mechanical life with a clear test condition, such as 100,000 cycles at 25 mA and 24 V DC, not just a number.
Order the same switch from two batches six weeks apart. Compare the actuator color, detent feel, and solder tail coplanarity. Small shifts in the plastic color often mean the molder changed the resin or regrind ratio, which can affect heat deflection temperature. Coplanarity differences over 0.1 mm hint at worn tooling or poor process control.
Internal lubricant migration is a common cause. Some factories over-apply silicone grease to mask a rough detent; the grease slowly creeps onto the contacts and hardens. Ask for a storage simulation: 1,000 hours at 85°C and 85 percent relative humidity, then test contact resistance. A shift above 30 milliohms indicates the grease or plating is not stable.
Conclusion
When you're comparing DIP switch suppliers, start with what's inside rather than what's on the datasheet. A switch that feels crisp today may not hold that feel after months in the field. The choice of plastic resin, the precision of the detent mechanism across every unit in a tube, and the thickness of contact plating all shape long-term behavior. A manufacturer that uses a lower-grade polymer or inconsistent detent tooling might pass a quick sample check, but the variations show up when a full production run is assembled. Plating that is too thin leaves contacts vulnerable to corrosion, and once oxidation starts, intermittent signals become a field failure that no amount of rework can fully erase. A supplier with tight control over these variables—where detents don't vary noticeably from switch to switch, and plating isn't skimped—prevents that slow creep of degradation.
But initial performance only gets you so far. Look for evidence of how switches age past the rated cycle count: ask for accelerated aging data or field returns from year three, not just spec-sheet endurance. Traceability matters too. If a batch fails, can the supplier trace it to the raw plastic lot or the plating line, or does the trail stop at a finished goods warehouse? A low rejection rate at final inspection is another quiet signal. It means upstream controls are working—tooling is stable, incoming materials are consistent, and assembly processes are predictable. These details, rather than marketing claims, tell you which manufacturer will actually keep your product reliable long after the purchase order is closed.
Contact Us
Contact Person: Anna lin
Email: [email protected]
Tel/WhatsApp: +86 13567768885
Website: https://www.kjele.com/